



Core Functions
1.Synchronous air tightness testing at multiple stations for accurate leak judgment
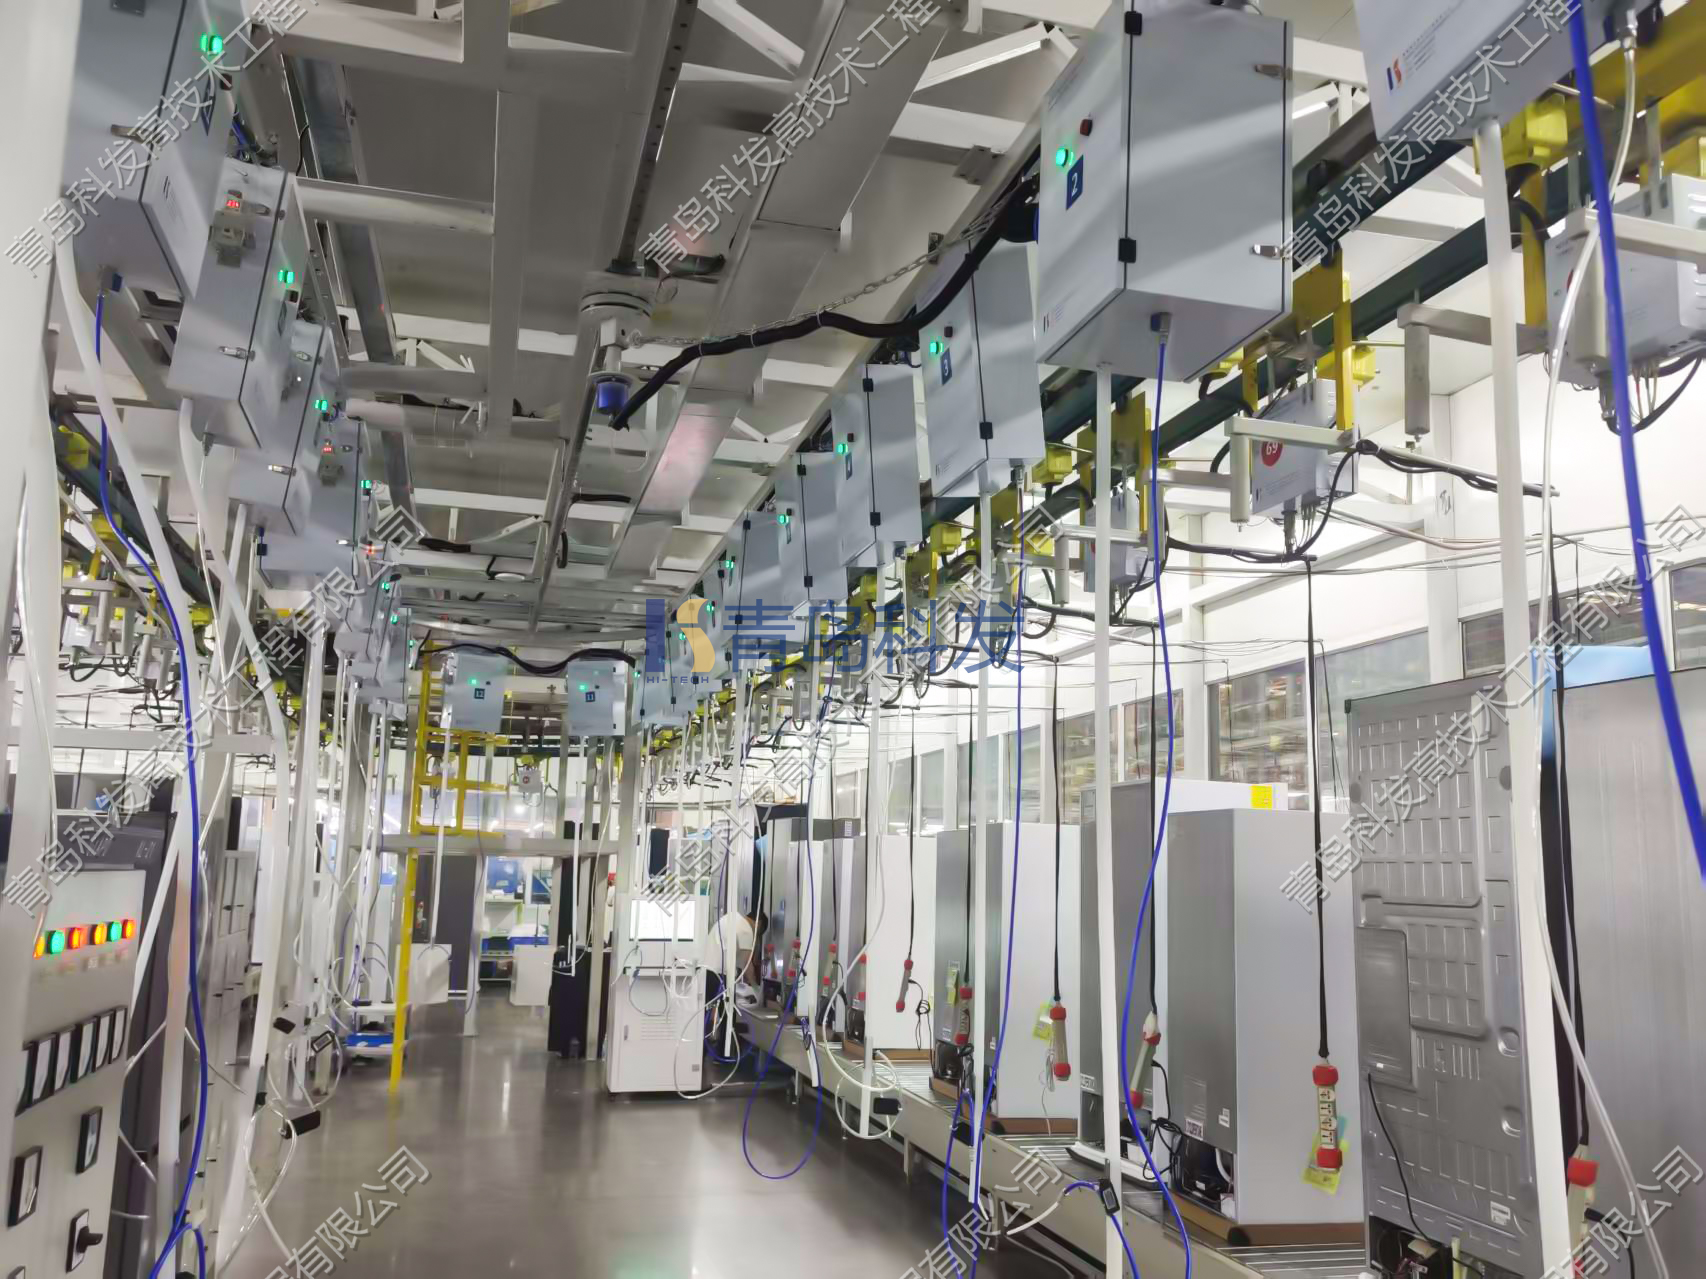
The system consists of software and 24 sets of independent air-tight hardware stations. Each single station independently completes the full process including inflation, pressure stabilization, pressure-holding leak test, pressure relief / reverse test. It collects real-time pressure data, compares and analyzes it against leak thresholds, and performs refrigerator LQC air pressure leak detection in accordance with preset pressure, timing sequence and pressure drop criteria to identify product leakage defects. It supports automatic connection of air supply pipes via cylinder sliding tables, triggers automatic alarms for connection failures, and allows retesting of leak NG products through remote controllers.
2.Flexible configuration of product templates for multi-product testing
Integrated with a model management and configuration module, the system supports creation, modification and deletion of customer models, reference models and judgment criteria, and enables binding of product barcodes with air tightness test schemes. Full sequence parameters such as inflation pressure, duration of each stage and leak thresholds can be customized to meet mixed-line testing requirements for different refrigerator models.
3.Multi-station parallel testing to match assembly line production tact time
The 24 test stations can run independently simultaneously. Scanning the product barcode automatically matches the corresponding air tightness parameters and executes the complete leak detection process automatically. The software realizes control of individual stations and centralized monitoring of the whole line status, adapting to continuous line flow and meeting batch inspection requirements of refrigerator production lines.
4.Complete data traceability and multi-condition query of test records
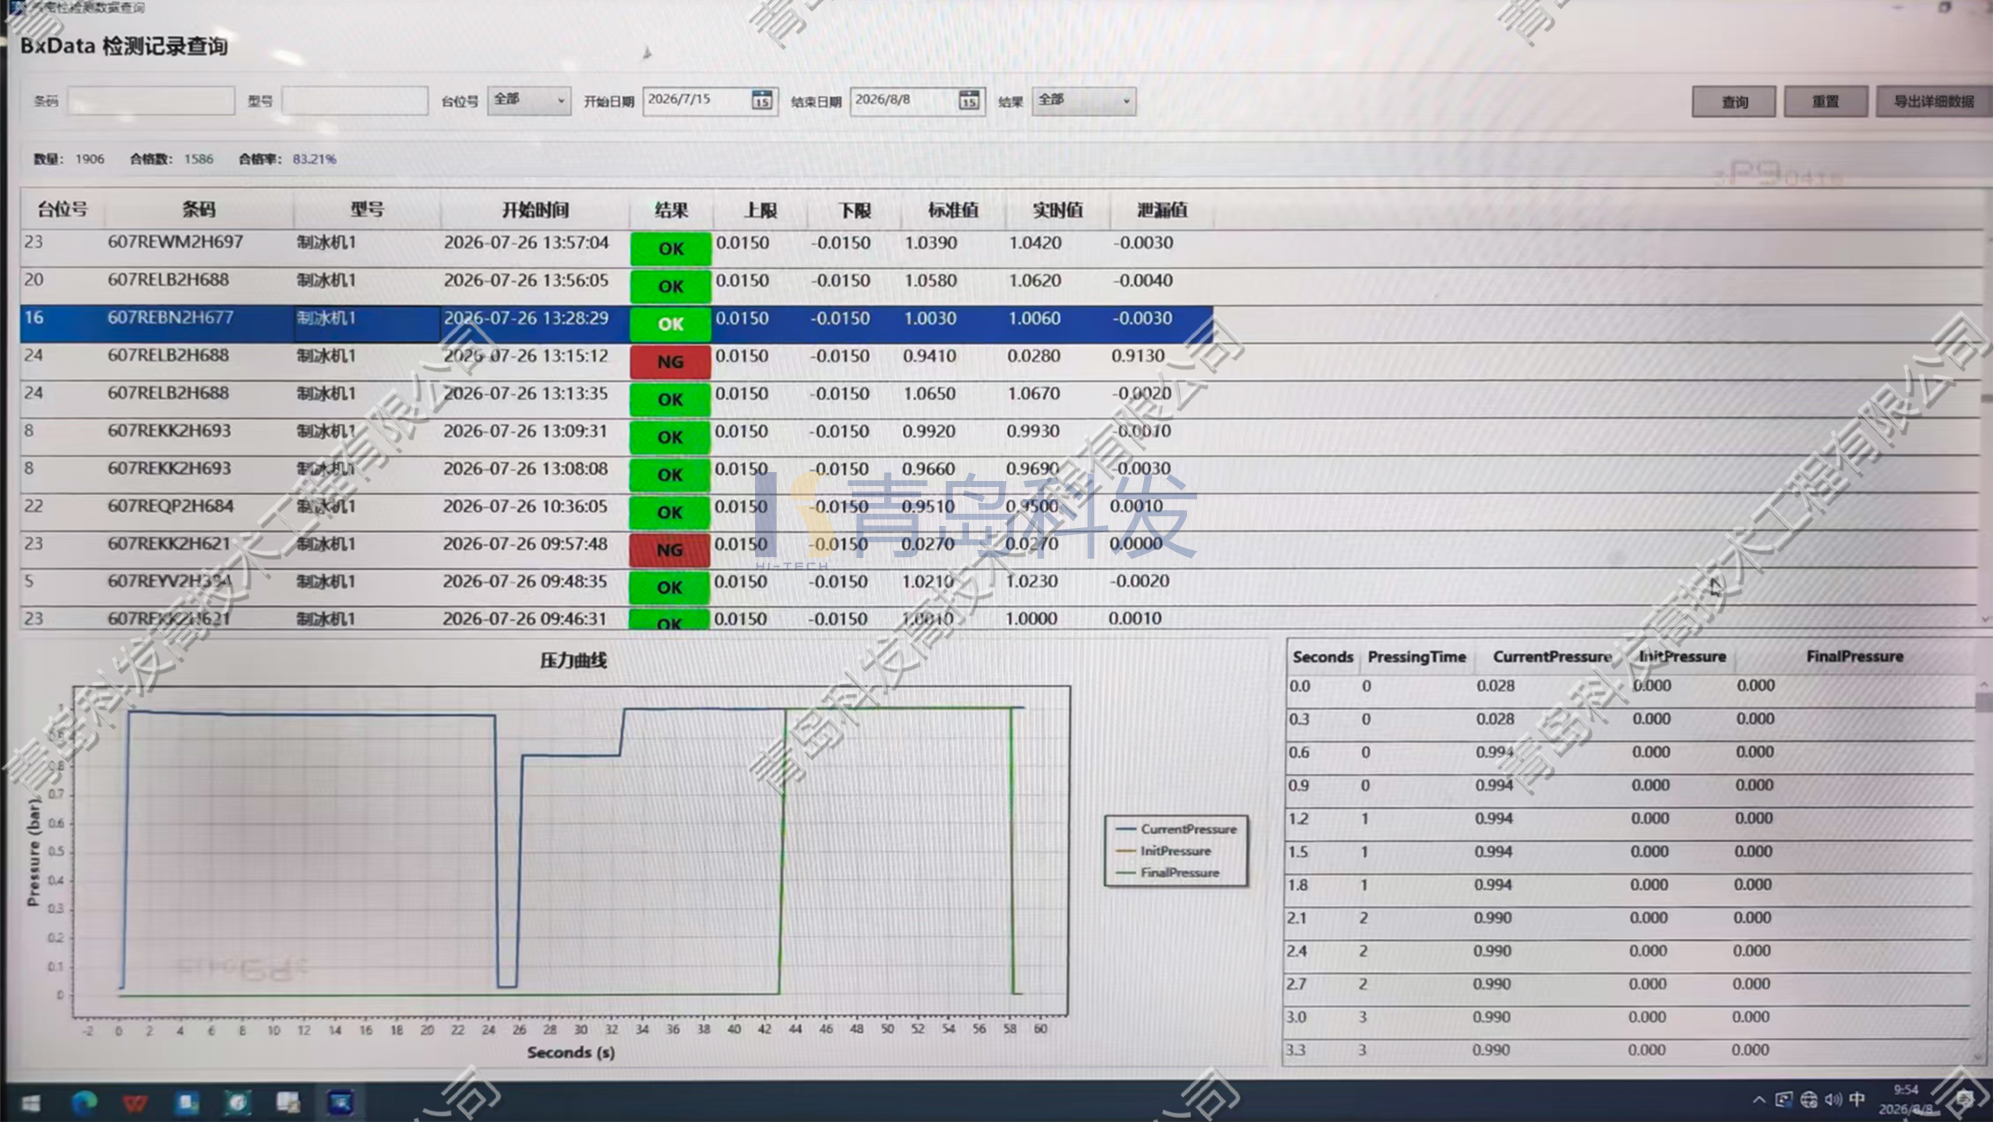
The system automatically stores raw test data from all stations. It supports multi-dimensional retrieval by time, product barcode, station and OK/NG test results. Full test details can be viewed and pressure variation curves can be replayed to assist root-cause failure analysis and achieve full-process quality traceability.
5.Visualized centralized monitoring with intuitive status feedback
The monitoring software displays set pressure, real-time pressure, test duration and operating status of all stations in real time, and fully presents pressure variation curves to facilitate on-site production control and equipment maintenance.
Project Features
High Integration: Integrates air-tight hardware testing, test sequence control, model parameter configuration, intelligent leak judgment, and data query & analysis.
High Flexibility: Supports rapid configuration and switching of air tightness parameters for multiple models. Test sequences and leak thresholds are flexibly adjustable to adapt to production line renovation and upgrade for various refrigerator products.
High Reliability: Equipped with industrial-grade hardware stations, it strictly implements the inflation-pressure stabilization-pressure holding test workflow. It incorporates alarm and retest logic for connection failures and abnormal leakage to ensure long-term stable operation of production lines.
Digital Management: Test data is automatically saved, pressure curves are replayable, and test records are searchable and traceable, realizing digital management of the entire air tightness testing process.
-
Type
-
Obtain solutions